
Every process, one works
From sheet to finished, inspected assembly — the machines, materials and tolerances a procurement engineer needs to see.
What we do
One works, every process from sheet to shipped assembly
A single accountable fabricator for the whole job — we cut the blank, form it, weld it, finish it and inspect it, so nothing falls between vendors or gets lost in a queue.
- 01
CNC laser & plasma cutting
Fibre-laser and plasma beds cut mild steel, stainless and aluminium up to 20 mm from your DXF or STEP — clean edges, tight nesting and repeatable blanks, prototype quantity through volume.
- 02
Press-brake forming & rolling
CNC press brakes to 170 tonne and plate rolling form brackets, enclosures, chutes and cylinders to drawing, with tooling and bend allowances proven on a first-off before a batch runs.
- 03
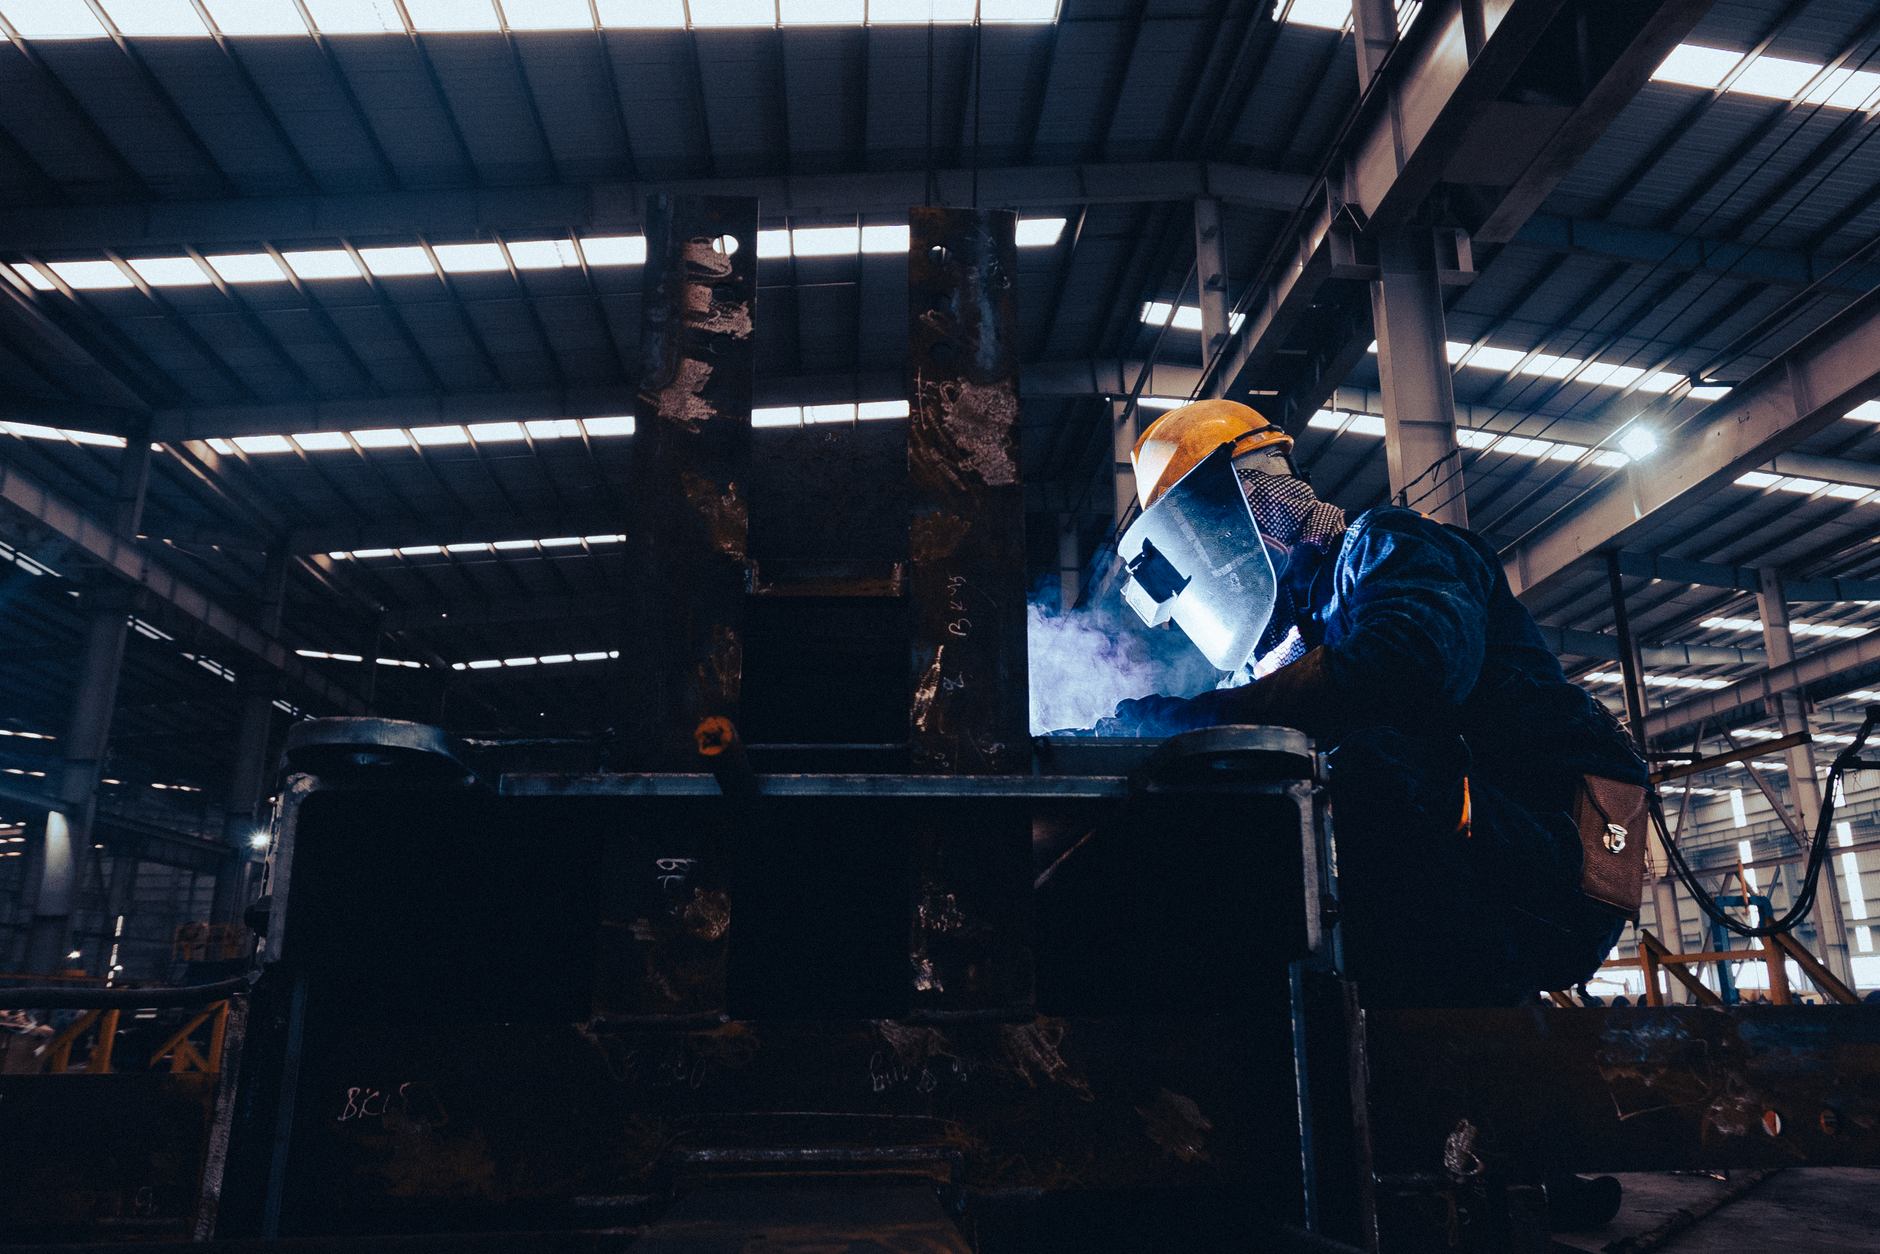
Coded welding & assembly
MIG, TIG and spot welding by ASME- and AWS-coded welders under an ISO 3834 welding-quality system — from stainless food-grade seams to structural steel weldments and full sub-assemblies.
- 04
Powder-coat & finishing
In-house shot-blast, pre-treatment and powder-coat line, plus brushing, passivation and silk-screen — parts leave finished, marked and packed, ready to install or fit straight to the line.
- 05
Machining & hardware
CNC milling and turning for machined features, plus PEM insertion, tapping and hardware fitting, so a fabricated part arrives complete rather than needing a second supplier.
- 06
Metrology & inspection
First-article inspection to your drawing, CMM and gauge measurement and documented dimensional reports — with certificates of conformance and material traceability per batch.
Shop capability
The spec sheet
Cutting
- Fibre laser
- 6 kW · to 20 mm mild steel
- Plasma
- HD plasma · to 25 mm plate
- Bed size
- 1.5 m × 3.0 m
- Also
- Shearing · sawing · notching
Forming
- Press brake
- CNC · to 170 tonne / 3.2 m
- Rolling
- Plate & section rolling
- Punching
- CNC turret punch
- Hardware
- PEM insertion · tapping
Joining & machining
- Welding
- MIG · TIG · spot
- Coding
- ASME IX · AWS D1.1
- Machining
- CNC mill & turn
- Standard
- ISO 3834-2 welding quality
Finishing & quality
- Coating
- Shot-blast · powder-coat line
- Stainless
- Brushing · passivation
- Tolerance
- to ±0.1 mm, CMM verified
- Materials
- MS · GI · SS 304/316 · Al
How a job runs
From your drawing to a finished, inspected part
One project engineer owns your job from RFQ to despatch, so you always know exactly where it stands.
Enquiry & DFM review
Send a drawing, a sample or a sketch. Our engineers review it for manufacturability — material, gauge, bends, weld access and finish — and return a costed quote, usually within two working days.
Tooling & first-off
We program the nest, prove the bend sequence and produce a first-off article, presented with a dimensional report for your sign-off before any batch is committed.
Fabrication
Approved jobs move to the floor — cut, form, weld and machine — run to a routing card with a coded welder and a fixture where the part needs one.
Finishing
Shot-blast, pre-treatment and powder-coat, brushing or passivation to your spec, then marking and labelling — parts leave the line finished, not raw.
Inspection & traceability
CMM and gauge checks against your drawing, a certificate of conformance and full material traceability with mill certs where the job calls for them.
Delivery
Packed to protect the finish and delivered on schedule or by kanban across the Klang Valley and to nine export markets — on the dates your build actually needs them.
Request a quote
Send us a drawing. We'll send back a plan.
Material, tolerance, finish and lead time — usually within two working days. You'll talk to an engineer who can scope the job, not a call centre.